Usbellows logo.png

EJMA Logo

US Bellows is a Standards Subscriber | Exp: Dec 31, 2026 | See ejma.org to check verification process
Celebrating over 20 years of EJMA membership

Metal Expansion Joint Codes and Standards: A Complete Reference Guide

September 10, 2026
Metal expansion joint

If you work with piping systems, you have probably heard engineers mention EJMA, B31.1, or B31.3. For anyone new to expansion joints or anyone trying to spec, purchase, or inspect one, these codes and standards are not just industry terminology. They are the rulebook that determines whether a joint passes inspections and performs safely over its intended service life. This article breaks down the major codes and standards that apply to expansion joints, what each one covers, and how they work together.

Metal expansion joints occupy an unusual position in piping systems. They are flexible components within otherwise rigid, code-governed piping, and they are expected to accommodate thermal expansion, vibration, and misalignment under pressure. A joint that is undersized, poorly welded, or rated for the wrong cycle life does not just underperform but can also fail under pressure during operation.

This is why expansion joints are subject to overlapping layers of requirements: an industry-specific design standard, an overarching piping or pressure vessel code, and often material and testing standards layered on top. Knowing which applies, and when more than one applies at the same time, is essential to a compliant, safe design. 
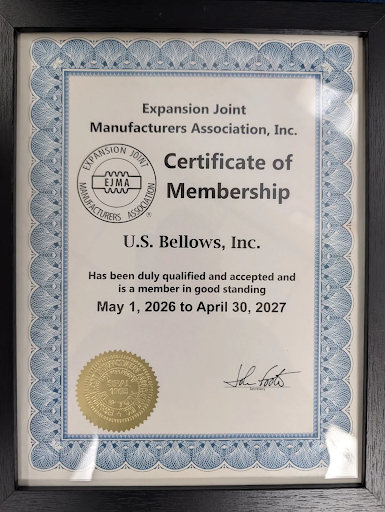
Us bellows ejma certification
US Bellows EJMA certification

EJMA: The Industry’s Foundational Design Standard

The Expansion Joint Manufacturers Association (EJMA) Standards are the primary technical reference for metal bellows expansion joint design. EJMA is a trade association document, not a government or ASME-issued code. It compiles decades of manufacturer testing data, design equations, and best practices into one reference. US Bellows has been an EJMA member since 2002, one of 14 member companies worldwide.

Among the topics EJMA’s Standards cover:

  • Design equations for bellows geometry, pressure capacity, and spring rates
  • Fatigue life (cycle life) prediction based on empirical test data
  • Guidance on multi-ply bellows, reinforced designs, and various bellows configurations
  • Manufacturing tolerances, bellows fabrication, and QC practices
  • Best practices for installation, shipping, and maintenance of bellows

The standard has continued to develop. More recent editions refine equations related to multiple plies, pressure calculations, membrane stresses, temperature effects, and harmonization with current ASME codes. EJMA is not a legally enforceable code. It does not dictate manufacturing, material stress allowables, examination, or quality assurance requirements. Those are set by codes such as ASME B31.3 or a customer’s own specification.

In short, EJMA defines how to design the bellows. It does not define the quality-control requirements needed to prove that it was built correctly. That is where ASME comes in.

ASME B31.3: Process Piping Code

For process piping, the kind found throughout refineries, chemical plants, and industrial facilities, ASME B31.3 is the governing code. B31.3 specifies requirements for materials, design, fabrication, assembly, erection, examination, inspection, and testing of piping systems.

Metallic Bellows expansion joints have a dedicated section: Appendix X. The overall approach adopts the EJMA Standards, with Code Committee modifications that turn EJMA’s industry recommendations into enforceable Code requirements for B31.3 piping. EJMA and ASME B31.3 are not competitors, but they are layered. A joint is generally engineered per EJMA’s design methodology, then verified against the Code requirements in B31.3 Appendix X for the overall assembly. 

Fatigue life is where this layering becomes practical for engineers. Bellows vendors often quote two different cycle lives for the same bellows: one calculated per EJMA, and one per ASME B31.3 Appendix X. The B31.3 number is typically lower because EJMA’s fatigue curve is a best-fit average based on test data, while ASME’s curve builds in the design margins expected of a pressure equipment code. 

B31.3 also drives requirements beyond the design calculations. Appendix X requires radiographic or dye-penetrant examination of the bellows tube for all metallic bellows, a requirement EJMA does not mandate. B31.3 also imposes its own hydrotesting requirements, testing the joint at the unit’s design temperature, which can require a higher test pressure than expected.

ASME B31.1: Power Piping

Where B31.3 governs process, chemical, and refinery piping, ASME B31.1 (Power Piping) governs piping in power generation facilities: steam lines and similar high-temperature, high-pressure service typical of power plants. Metal expansion joints used in these systems are often specified against B31.1. The applicable design margins and testing requirements can differ, so confirm which code governs a given system before assuming B31.3 rules apply.

ASME Section VIII: Pressure Vessels

Metal expansion joints are not limited to piping. They also appear on pressure vessels and heat exchangers, accommodating differential thermal expansion between shells and tubes. This was historically covered by Section VIII, Division 1, Appendix 26, for bellows expansion joints on vessels operating above 15 psig, which took a different design approach than B31.3’s Appendix X.

As part of ASME’s Section VIII Reshape initiative, the design methodology for thin-walled bellows expansion joints in Appendix 26 was recognized as essentially identical to the method in Division 2, paragraph 4.19. Starting with the 2023 edition, the common design calculations were consolidated into Division 2, with Division 1 referring to that method. Division 1 still governs inspection, testing, and material and certification requirements, but now refers to Division 2 for the underlying calculation methods, as part of ASME’s broader effort to unify calculations across both divisions.

For a bellows on a pressure vessel today, the governing calculations are in Division 2, while Division 1 (Part UEB) covers fabrication, inspection, and certification requirements. Confirm which Code edition a project is built to, since older equipment may still be certified under the legacy Appendix 26 rules.

Supporting Material and Testing Standards

Beyond the three main piping and vessel codes, several supporting standards apply to metal expansion joint projects:

  • ASME B16.5 and B16.47: flange dimensional standards, since metal expansion joints are almost always flange-connected into a piping system
  • ASME B&PV Section V: nondestructive examination methods (radiography, dye-penetrant testing), directly relevant to the bellows tube inspection required under B31.3 Appendix X
  • ASME B&PV Section IX: welding qualification requirements for the shop welds that join bellows elements, end connections, and reinforcing members

They are the standards a metal bellows is fabricated and inspected against once the EJMA and ASME design work is complete.

Putting It Together: What This Means for Your Project

For specifying, purchasing, or inspecting a metal expansion joint, a few practical points apply:

  1. Identify the governing piping code first: B31.3, B31.1, or Section VIII. This determines which Appendix and which testing and examination rules apply.
  2. Do not assume EJMA compliance equals Code compliance. EJMA governs the bellows design methodology. The applicable ASME code governs materials, fabrication, examination, and testing of the finished assembly.
  3. Confirm NDE and welding requirements up front. Radiographic or dye-penetrant examination of the bellows tube, along with Section IX-qualified welding, separates a Code-compliant metal joint from one that only looks compliant.
  4. Check for secondary standards or customer specifications relevant to expansion joint fabrication, quality, and testing.

Navigating overlapping codes is specialized work. If it is unclear which standards apply to an application, or a joint needs to be engineered to satisfy multiple codes at once, that is worth discussing with an expansion joint manufacturer early in the design process.

Note: Always consult the current edition of the applicable code and a qualified engineer for project-specific design decisions.

Talk to a Professional

Unsure which codes and standards apply to your expansion joint project? Schedule time with an engineer for a review of your application, or explore our full range of expansion joint solutions to see tied, universal, hinged, and gimbal designs.

Ready to move forward? Request a quote, and our engineering team will follow up with pricing and lead time for your application.


Read More
Braided Flexible Hose vs. Tied Expansion Joint: Selection Guide

September 1, 2026
Braided Hose in the facility
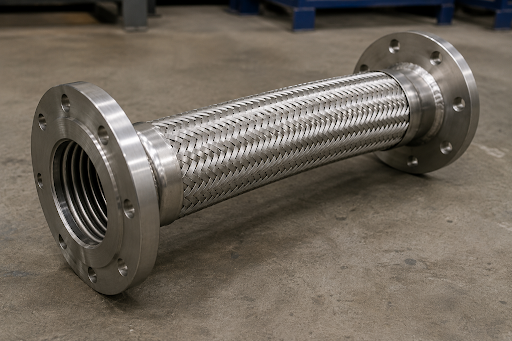
Braided Flexible Hose
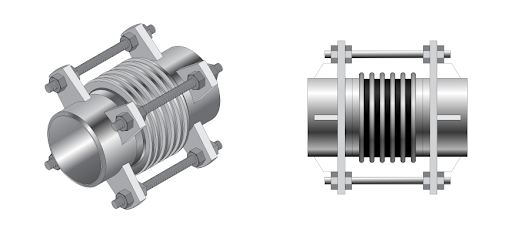
Universal expansion joint with tie rods

Braided flexible hose and tied expansion joints are both used to restrain pressure thrust while allowing movement in a piping system, and the two are often confused. Selecting the wrong product can result in inadequate movement capacity, unrestrained pressure thrust, or a connection that does not fit the available space envelope. This guide explains what each product is, how each restrains pressure thrust, what movement each is built to handle, and how to decide between them.

What Is a Braided Flexible Hose?

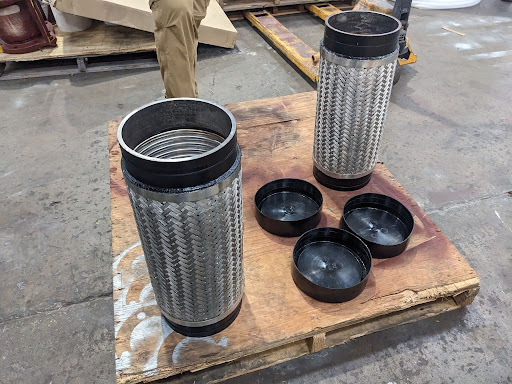
A braided flexible hose consists of a corrugated metallic hose core surrounded by one or more layers of metallic wire braid. The corrugated hose provides flexibility, allowing the assembly to bend or move laterally, while the external braid provides reinforcement and contains the pressure thrust generated by internal pressure.

What Is a Tied Expansion Joint?

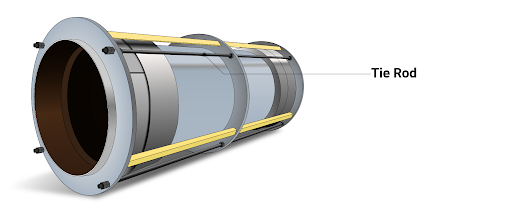
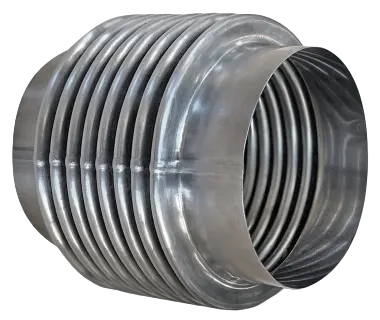
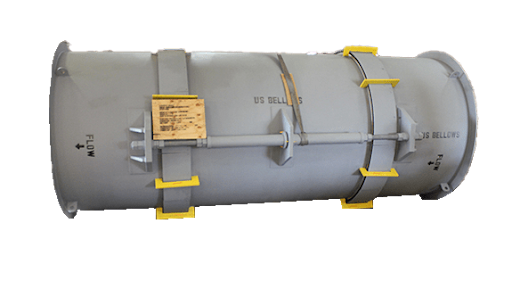
A tied expansion joint is a metal bellows expansion joint fitted with tie rods that run between the assembly’s end flanges through tie-rod lugs. The bellows provide flexibility, allowing the joint to absorb lateral or angular movement, while the tie rods restrain the pressure thrust generated by internal pressure and keep that force from acting on the connected piping or equipment.

Braided flexible hose

How Each Restrains Pressure Thrust

A tied expansion joint and a braided flexible hose can serve similar functions, particularly where lateral movement is required while pressure thrust must be restrained. A tied expansion joint uses tie rods connected to the assembly through tie-rod lugs. The rods restrain pressure thrust while allowing the intended lateral or angular movement. A braided flexible hose achieves the same result differently: the corrugated hose provides flexibility by bending along its length, while the external braid resists pressure thrust and limits axial movement.

When a Tied Expansion Joint Is the Better Choice

A tied expansion joint design, like PTP’s tied universal expansion joint, is generally preferred when the application requires:

  • Larger, controlled lateral movement
  • A short overall assembly length
  • Precisely defined movement capability
  • High axial or lateral structural loads
  • Large pipe diameters
  • Specific spring-rate requirements
  • Engineered movement under thermal expansion
  • Specialized liners, covers, or flow-control features

When Braided Flexible Hose Is the Better Choice

A braided flexible hose is generally preferred when the application requires:

  • Installation in a space too tight for tie-rod hardware and its movement envelope
  • Vibration isolation at rotating or reciprocating equipment such as pumps, compressors, or turbines
  • Only a relatively small amount of lateral movement
  • Tolerance for limited installation misalignment between equipment and piping
  • A simpler assembly that is faster to manufacture, inspect, and replace
  • A connection that is removed and replaced periodically, such as at equipment that is pulled for service

Selection Guide

Choose Braided Flexible Hose When Choose a Tied Expansion Joint When
Movement is relatively small Larger lateral movement is required
Vibration isolation is important Movement must occur within a short, defined length
A flexible equipment connection is needed Movement and spring forces must be accurately controlled
Space or installation simplicity is important The application involves larger piping or significant system loads
Pressure thrust needs to be internally restrained Engineered accessories such as liners or covers are required
A simple, replaceable assembly is preferred A specific spring rate is required


Talk to a Piping Specialist

Not sure whether your application calls for a braided flexible hose or a tied expansion joint? Schedule time with an engineer for a review, or explore our full range of expansion joint solutions to see tied, universal, hinged, and gimbal designs in detail.

Ready to move forward? Request a quote, and our engineering team will follow up with pricing and lead time for your application.

Read More
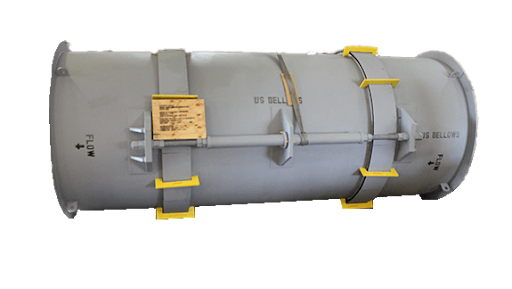
116″ Universal Expansion Joint for a Water Supply System in California

August 31, 2026

116" Universal Expansion Joint for a Water Supply System in California

Type: Universal Expansion Joint
Size: 116″ in diameter/60″ long
Material: AL6XN Stainless Steel/Carbon Steel
Design: 100°F at 220 PSIG, 9″ axial compression
Testing: Dye penetrant, radiographic, and hydro tested

U.S. Bellows custom-engineered and manufactured this impressive 116″ reinforced universal expansion joint for a water supply system in California. Measuring 116″ in diameter and 60″ in overall length, the unit demonstrates U.S. Bellows’ ability to design and fabricate large-diameter expansion joints for demanding infrastructure applications.

The bellows and pipe spool were fabricated from corrosion-resistant AL-6XN stainless steel, while the flanges were manufactured from carbon steel. The bellows were reinforced with AL-6XN round bar in the convolutions to contain the pressure at that volume, as the expansion joint was designed for an operating temperature of 100°F at 220 PSIG and engineered to accommodate 9″ of axial compression.

Before shipment, the completed assembly underwent extensive nondestructive examination and performance testing, including dye penetrant testing, radiographic testing, and hydrostatic testing. These quality-control measures verified the integrity of the welds and confirmed that the expansion joint met the project’s performance requirements.

U.S. Bellows has designed and manufactured engineered expansion joints since the 1960s. The company provides custom metallic, fabric, and rubber expansion joints, along with clamshell bellows, pressure-balanced assemblies, and fabricated ductwork for complex piping and ducting systems. Its engineering capabilities include design in accordance with EJMA equations and applicable ASME standards, as well as in-house finite element analysis for specialized applications.

As a longtime member of the Expansion Joint Manufacturers Association, U.S. Bellows combines specialized engineering, extensive fabrication capabilities, comprehensive testing, and field support to deliver reliable solutions for water infrastructure, refining, chemical processing, power generation, marine, offshore, and pipeline applications. The company also offers emergency engineering, manufacturing, inspection, installation support, and repair services to help customers minimize downtime during critical plant outages and system failures.

Read More

All About Braided Flexible Hose: Construction & Applications

August 24, 2026
Braided Flexible Hose

In many applications, a tied expansion joint is used to accommodate lateral movement while restraining pressure thrust within the assembly. However, when greater flexibility is needed due to space limitations, vibration, or equipment movement, a braided flexible metal hose can provide a simpler and more practical alternative.

What Is a Braided Flexible Hose?

A braided flexible hose generally consists of a corrugated metallic hose core surrounded by one or more layers of metallic wire braid. The corrugated hose provides flexibility, allowing the assembly to bend or move laterally, while the external braid provides reinforcement and contains the pressure thrust generated by internal pressure.

The braid serves as the primary structural element of the assembly. When the corrugated hose is pressurized, the pressure acting over its effective area generates a thrust, the same force a tied expansion joint must manage. The braid restrains that thrust and limits axial extension of the hose, performing a function similar to the tie rods on a tied metallic expansion joint. 

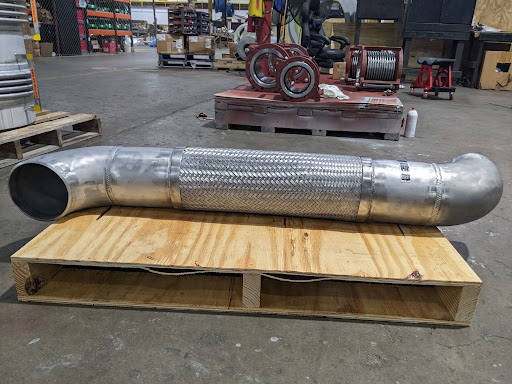
Braided Hose in the facility

When Braided Flexible Hose Can Be Preferred

For the right application, braided hose offers several practical advantages over a tied expansion joint.

  • Simpler Construction – A braided hose generally consists of just the braid and weld collars that are faster to manufacture, install, inspect, and replace.
  • Compact Installation – Flexible hose assemblies are well suited to installations where space is genuinely tight. Aerospace piping is a good example: there’s often no room for tie-rod hardware and its required movement envelope, so a properly routed flexible hose delivers the needed movement in a far more compact arrangement.
  • Vibration Isolation – One of the most common reasons for selecting a braided flexible hose is to isolate equipment vibration. Rotating and reciprocating equipment like pumps, compressors, and turbines transmits vibration into connected piping. A properly designed flexible hose absorbs that movement and reduces how much mechanical vibration reaches the rest of the system.
  • Small Lateral Movements – When only a relatively small amount of lateral movement is required, a flexible hose is often more practical than a tied expansion joint. The hose accommodates movement through bending distributed over its flexible length. Increasing the available length and choosing the right installation configuration let it accommodate movement without overstressing the corrugations. For larger movements, an engineered expansion joint remains the more controlled, compact solution.
  • Installation Misalignment – A flexible hose can absorb limited misalignment between equipment and piping, useful when field conditions make perfect alignment difficult. It should not, however, be used to correct severe misalignment or poor installation practice, since permanent misalignment consumes part of the hose’s available flexibility and can shorten service life.
  • Easier Replacement – Flexible hose assemblies are typically straightforward to remove and replace, which is valuable where the flexible connection is a maintainable component or where equipment is periodically pulled for service.
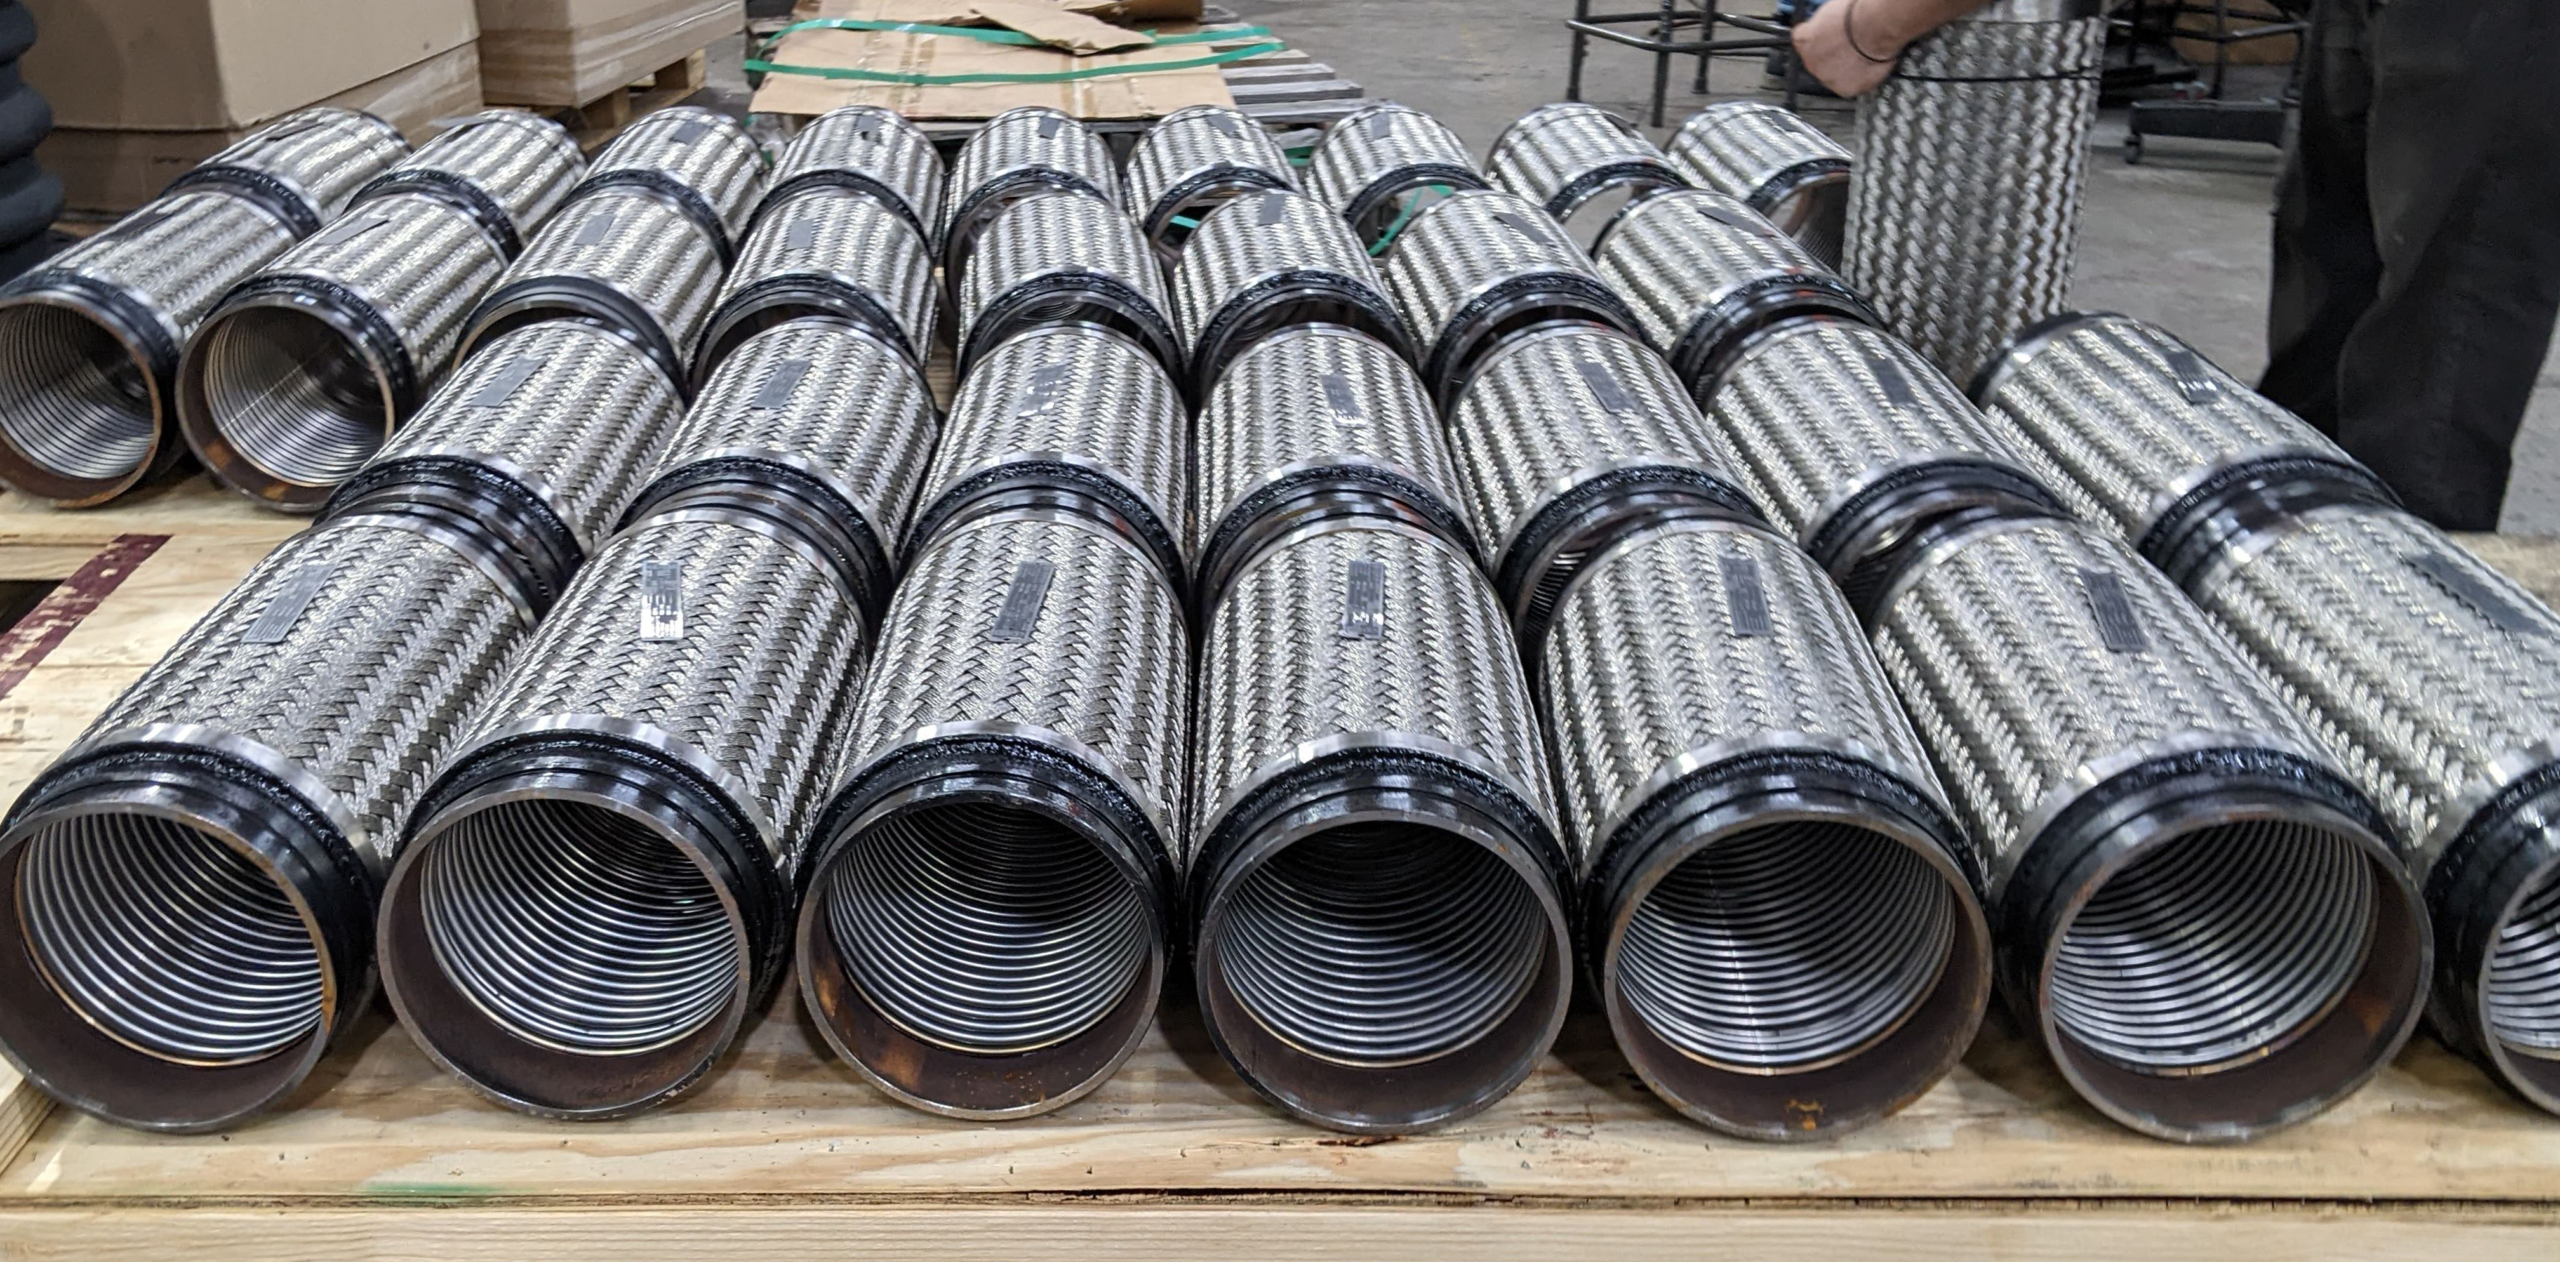
Braided Hose assemblies in production

Getting the Flexible Length Right

A common mistake in flexible hose design is making the hose too short. Flexible hose accommodates lateral movement through bending, not by stretching axially. If the hose is too short, its bending radius becomes tighter, and the corrugations see higher stress, which can significantly reduce fatigue life. A longer flexible length spreads that movement over a larger section of hose. The same movement-calculation discipline applies to expansion joints; see our buyer’s roadmap for calculating movement requirements for the equivalent process on the tied-joint side.

Installation Considerations

Even a correctly designed flexible hose can fail prematurely if installed incorrectly. The hose should be installed so that movement occurs in the intended plane without introducing excessive torsion. Torsion is especially damaging because corrugated hose is designed to flex through bending, not twisting. 

Pressure Thrust and Piping Loads

One of the major advantages of both braided hose and tied expansion joints is their ability to contain pressure thrust. In an untied bellows expansion joint, internal pressure creates thrust that must normally be resisted by anchors or other structural components. A tied expansion joint uses tie rods to contain that thrust within the assembly; a braided hose’s braid does the same job, restraining axial extension of the corrugated core and transferring pressure-induced forces between the end fittings. Thrust restraint doesn’t mean zero load on connected equipment; however, hose stiffness, bending forces, weight, dynamic loads, and installation geometry all still need to be considered and may still call for properly sized pipe supports nearby.

Typical Applications

Braided flexible hose assemblies are commonly used for:

  • Pump suction and discharge connections
  • Compressor connections
  • Vibration isolation
  • General equipment connections
  • Skid piping
  • Small thermal movements
  • Limited lateral movement
  • Piping misalignment
  • Connections where equipment must be periodically removed
  • Space-constrained installations  –  aerospace piping is a prime example, where a conventional expansion joint would be unnecessarily complex

These assemblies show up across data centers, oil & gas, petrochemical, and other process industries; which product gets specified usually comes down to available space and required movement rather than the industry itself.

Design Standards

Flexible metal hose assemblies are designed and manufactured using recognized industry practices for metallic hoses. Organizations such as NAHAD provide guidance on fabrication, testing, installation, and application. The piping system itself may also fall under an applicable piping code, such as ASME B31.1 or ASME B31.3. This differs from metallic bellows expansion joints, which are commonly designed using EJMA methodology alongside applicable piping or pressure design requirements. One practical consequence: braided hose doesn’t have an equivalent standard for estimating service life the way EJMA-designed tie rods do, so inspection and replacement intervals are typically set by application experience rather than a published life calculation.

Frequently Asked Questions

Does a braided flexible hose allow the same movement as a Tied Expansion joint?
This is a common misconception worth clearing up: neither a braided flexible hose nor a tied expansion joint accommodates axial (straight-line stretching) movement; both are restrained against that by design. What they allow is lateral and angular movement: the hose through bending along its flexible length, the tied joint through controlled bellows deflection.

How long does a braided flexible hose last compared to a tied expansion joint?
There’s no industry standard or code for calculating a braided hose’s expected life cycle the way EJMA methodology allows for tied, engineered expansion joints. In practice, tie rods and bellows designed to EJMA guidelines are generally expected to outlast a braided hose in continuous service, so periodic inspection and a planned replacement interval are recommended for hose assemblies.

Which industries use braided flexible hose most?
It shows up across data centers, oil & gas, petrochemical, and general process industries, plus space-constrained fields like aerospace where there simply isn’t room for tie-rod hardware. The deciding factor is usually available space and required movement, not the industry itself.

Talk to a PTP Piping Specialist

Not sure whether your application calls for a braided flexible hose or a tied expansion joint? Schedule time with an engineer for a review, or explore our full range of expansion joint solutions to see tied, universal, hinged, and gimbal designs in detail. 

Ready to move forward? Request a quote, and our engineering team will follow up with pricing and lead time for your application.

Read More
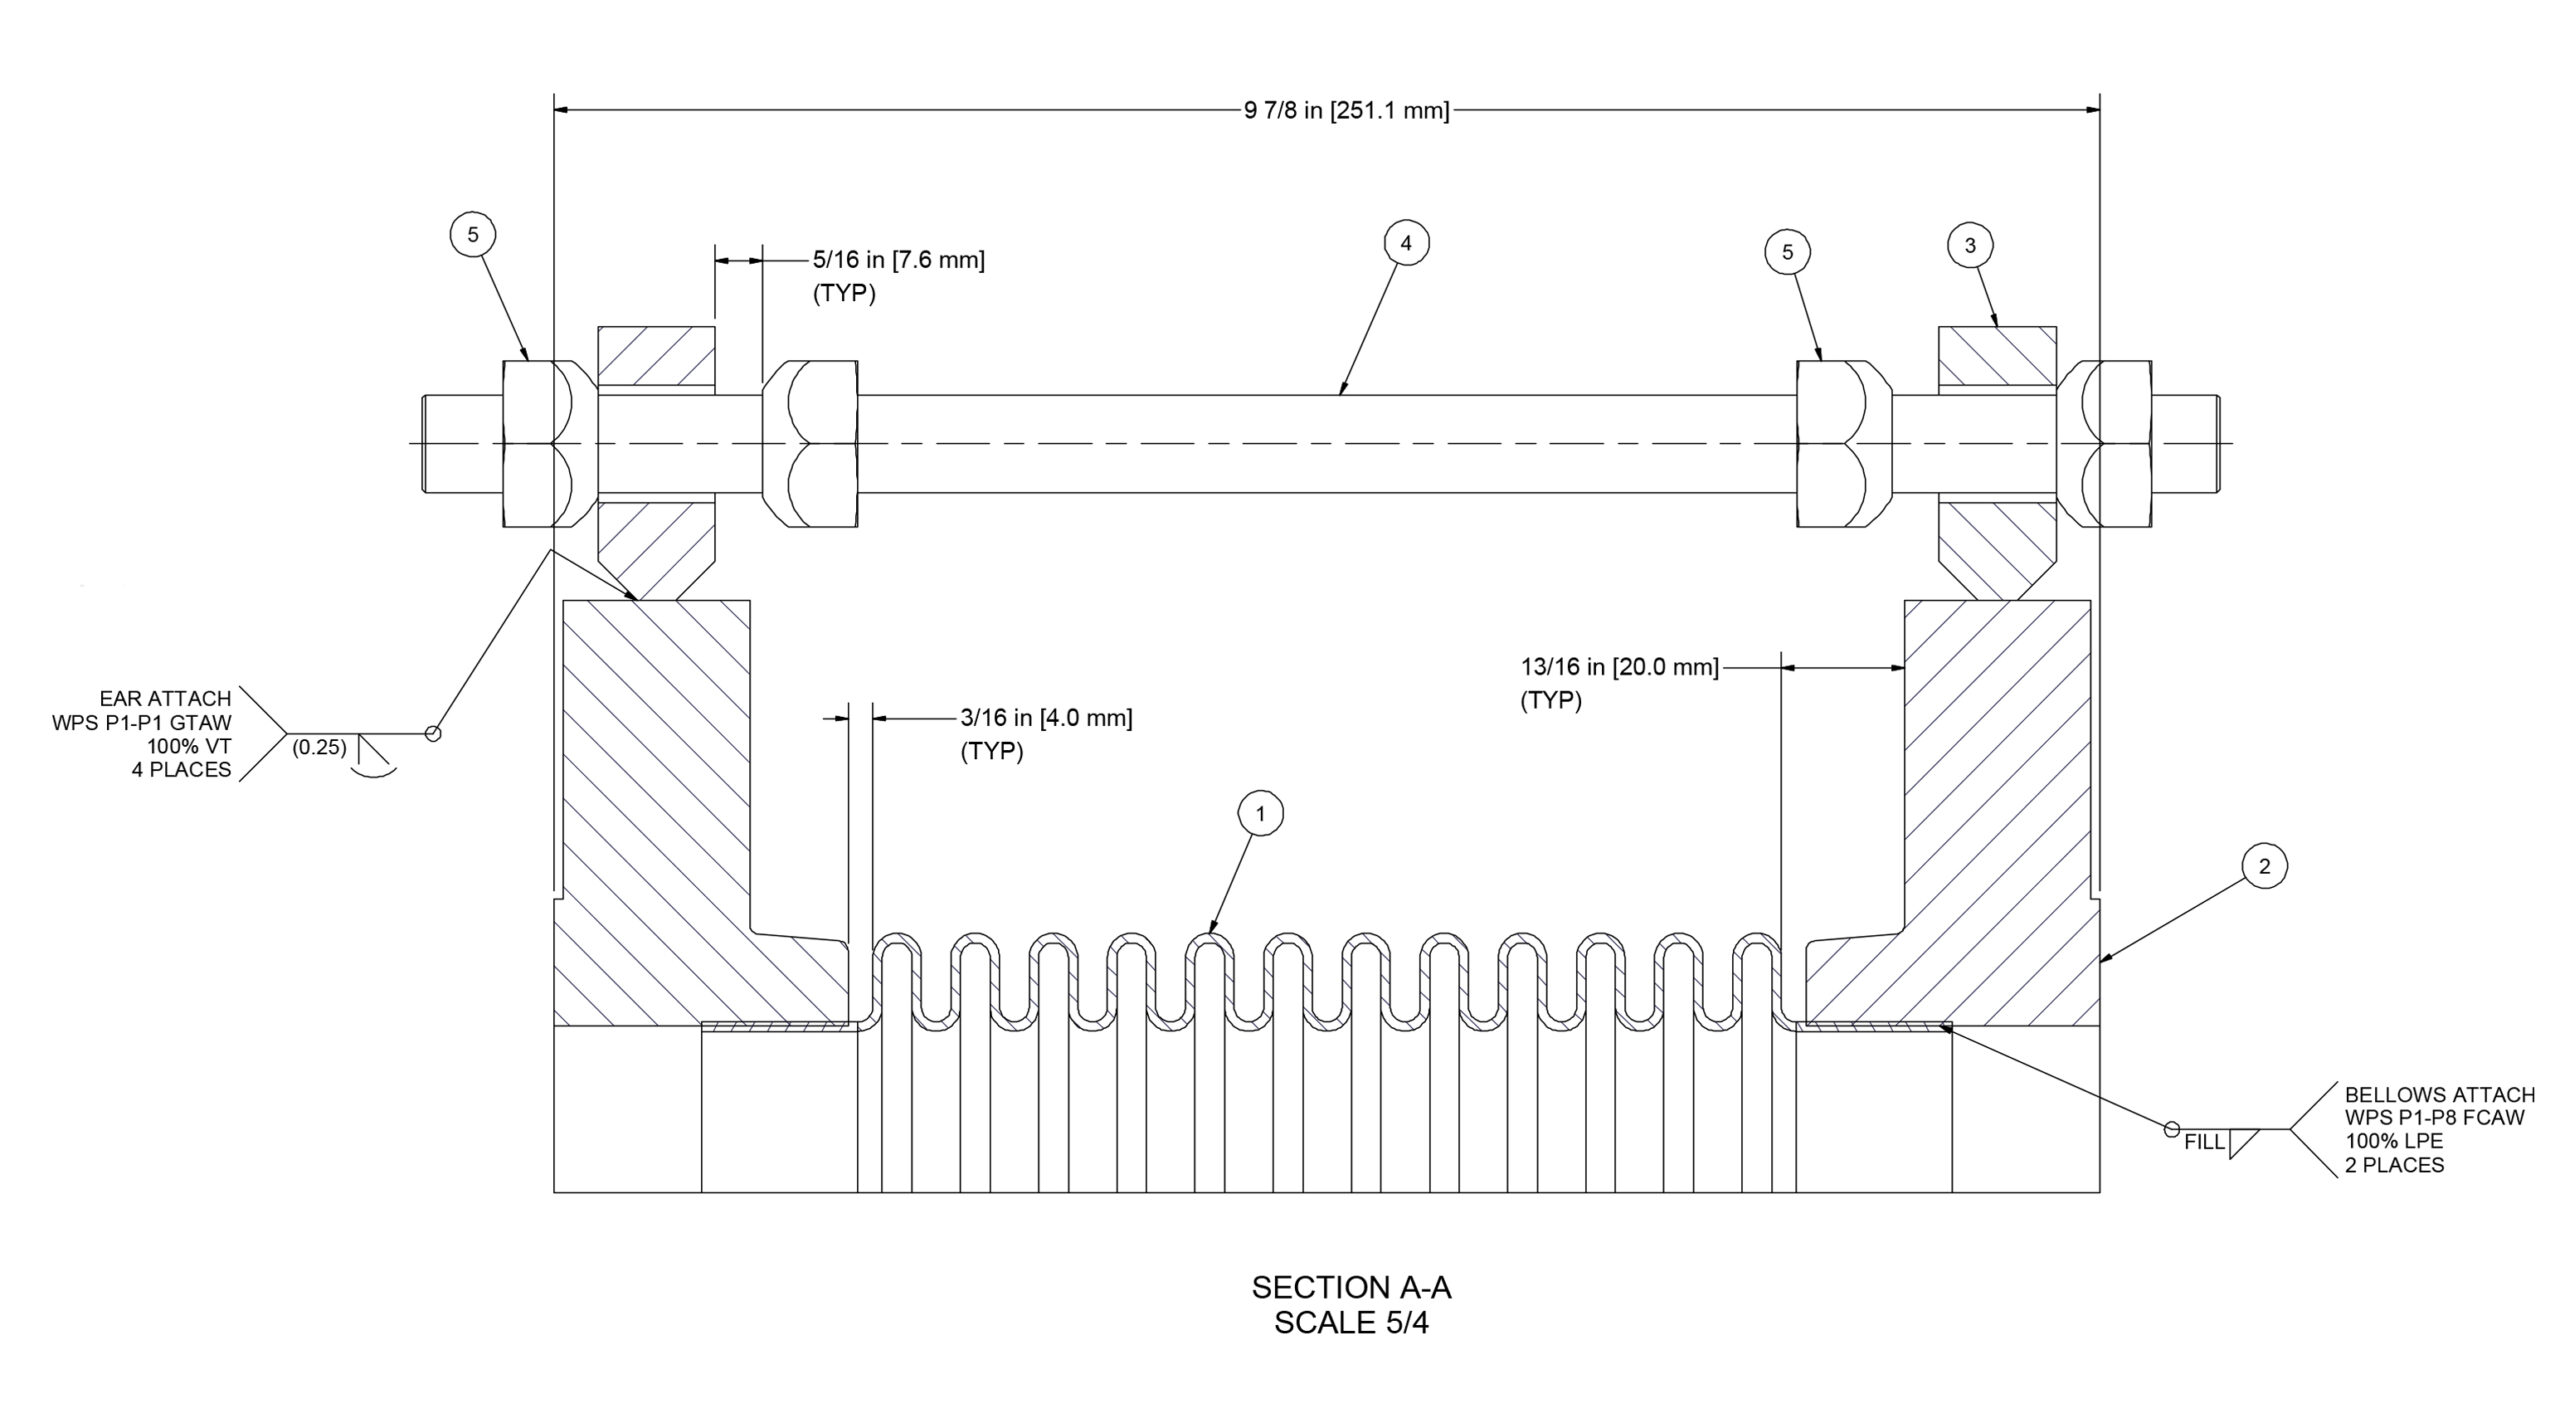
How the Clearance Between the Nuts and Lugs Works on a Tied Expansion Joint

August 7, 2026
 Tie-rods with hex nuts and lugs on a metallic expansion joint
Tie-rods with hex nuts and lugs on a metallic expansion joint

In a restrained expansion joint assembly, the hex nuts on a tied expansion joint are intentionally positioned with a measured gap between the nut and the lug. Customers frequently ask whether this clearance is necessary. The answer is yes – it is a critical design feature that allows the expansion joint to function as intended while protecting the bellows from excessive loads.

While “control rod” and “tie-rod” are sometimes used interchangeably in the expansion joint industry, they serve different functions. Tie-rods are meant to continuously restrain full pressure thrust and permit only lateral movement during normal operation (i.e, there’s no gap in between the rods and nuts). Control rods are meant to prevent over-extension or compression (i.e, there’s a gap in the rods and nuts),  and are designed to contain the full pressure thrust in case of an anchor failure.

This article explains the purpose of the clearance between the nuts and the lugs and how it is determined during design. We will also look at consequences for the piping system when it is altered in the field. 

 Tie rod assembly on a metallic expansion joint
Tie rod assembly on a metallic expansion joint

What Is the Nut and Lug Clearance?

An expansion joint is designed to absorb movement in a piping system. As the line heats up and cools down, the pipe expands and contracts, and the bellows compress and extend to absorb that movement, preventing it from transferring to the surrounding piping and equipment.

The tie rod assembly is the hardware that controls this movement (normally lateral movement). It consists of three components:

  • Tie rods: Rods that span the joint from one end to the other
  • Ear plates (lugs): plates welded to each end of the joint that the rods pass through
  • Hex nuts: positioned on the rods based on the movement at the lugs

Tie Rod, Limit Rod, or Control Rod?

In the field, the terms tie rod, limit rod, and control rod are often used interchangeably, and they can refer to hardware that looks nearly identical: a threaded rod passing through lugs, held by hex nuts. They are, however, technically different components, and the distinction matters when specifying an expansion joint. 

A tie rod continuously restrains the full pressure thrust of the system during normal operation and permits only lateral deflection. A limit rod allows the joint to move within its designed range, limiting axial expansion or compression, and restrains the pressure thrust only in the event of an anchor failure. A control rod is used on universal expansion joints to limit and control the movement of the assembly. The correct term depends on the function the rod performs, and each is custom-designed based on the pressure and load forces of the specific application.

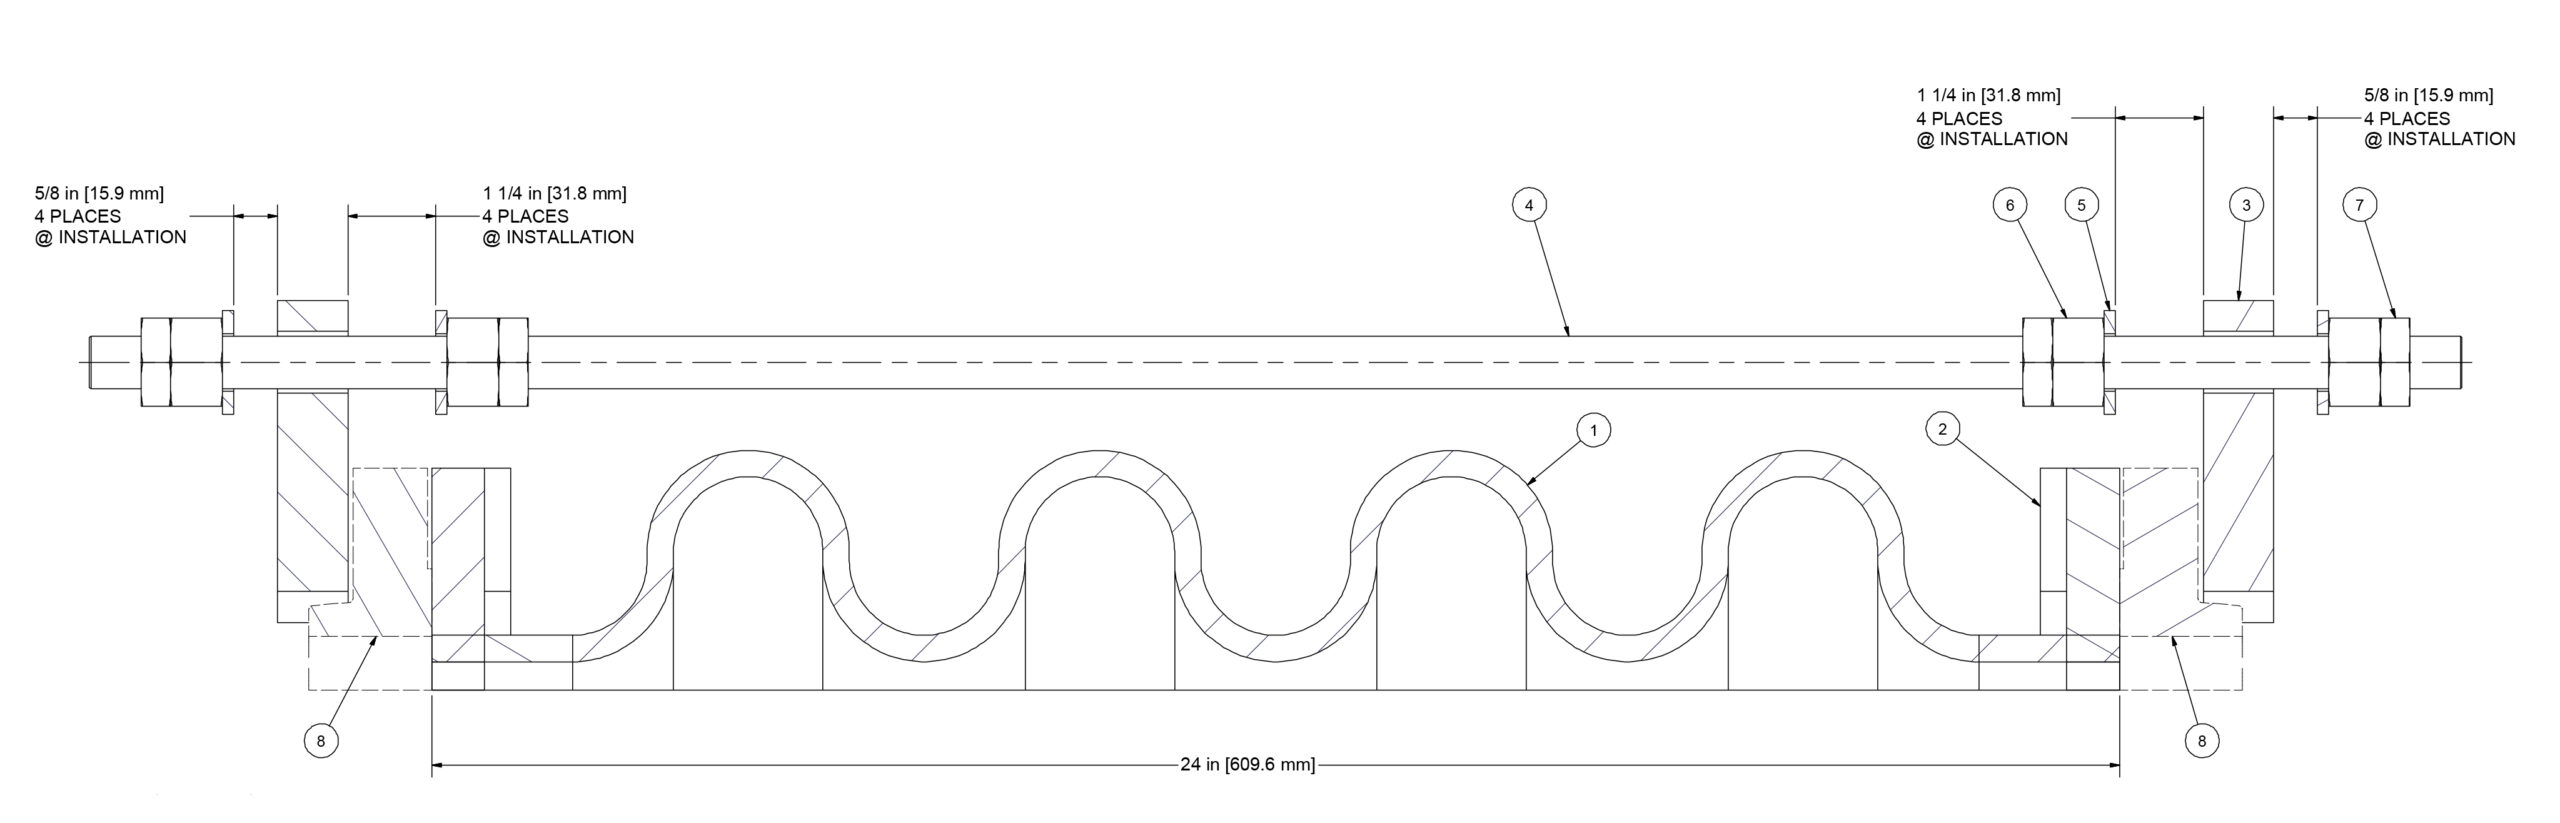
The clearance is the deliberate gap left between the hex nut and the lug. That gap allows the bellows to move and compress without damaging the equipment. Within it, the joint moves freely as the pipe expands and contracts, and the gap defines the limit of that movement. 

Single metallic expansion joint
Universal expansion joint with tie rods

–>

How Is the Gap Calculated?

The clearance is not a standard dimension. It is unique to each expansion joint design and is determined by the engineering team based on the movement requirements of the application.

Designed for 2.25″ Compression and 1.25″ expansion for Single EJ

Single expansion joints – For a single expansion joint, the engineering team divides the total travel requirement in half and sets that value as the clearance on each side of the lug. For example, if a joint is designed for 2 inches of total axial travel, that travel is split across the two sides: a 1-inch gap is set between the nut and the lug on one side, and a 1-inch gap on the other. The joint is free to move within these clearances, and the nuts stop it from traveling beyond them.  

Designed for 5/8" Compression EJ
Designed for 5/8″ Compression EJ

Universal expansion joints – A universal expansion joint consists of two bellows separated by a center pipe section, or spool, and is designed to absorb large amounts of lateral deflection. Because the movement is distributed across two bellows, the clearance cannot be set by simply dividing the travel in half. The engineering team determines the clearance dimensions specifically for each design.

Note – These principles apply to all expansion joint types. Including metallic, fabric, and rubber expansion joints.

What Happens When the Gap Is Set Wrong?

Improper installation in either direction puts the system at risk.

  • When the Gap Is Closed (Nuts Tightened Against the Lugs)

Tightening the nuts against the lugs prevents the expansion joint from moving axially. The joint can no longer absorb the expansion and contraction of the pipe, and the thermal stress is transferred to an anchor or equipment in the piping system, which may cause a failure on either of those structures.

  • When the Clearance Exceeds the Design Specification

Excessive clearance allows the expansion joint to move beyond its designed travel. If the joint is not designed to handle that level of movement, this can lead to premature failure of the unit.

Set in the Shop, Guided by the Drawings

Every assembly is fabricated and assembled at our facility before shipping. Customers generally do not need to perform any field welding on these assemblies. Where field work is required, we provide the drawings needed to guide correct installation.

Takeaway

The clearance gap between the nuts and the lugs is part of the design. It allows the expansion joint to move as intended and defines the limit of that movement. The nut positions on a new assembly are set to the design dimensions and should not be adjusted during installation or maintenance.

If you have questions about the correct clearance for your application, contact US Bellows or schedule a meeting with an engineer.


Read More

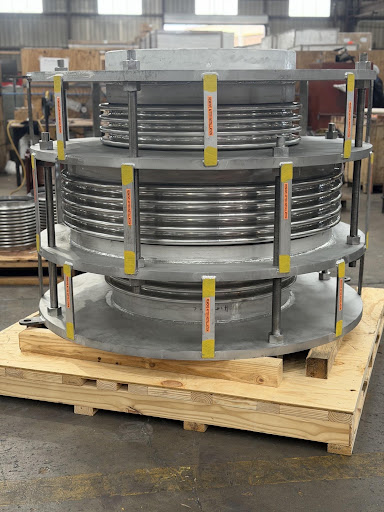
Emergency-Fabricated 36” NPS Pressure Balanced Expansion Joint for Uranium Processing Application

July 30, 2026

When one of the world’s leading uranium producers faced an urgent need for a critical piping component at their Canadian mining operations, US Bellows delivered. Engineered and fabricated on an emergency rush basis, this 36” NPS Inline Pressure Balanced Expansion Joint is a testament to our team’s ability to respond fast without compromising quality.

Completed expansion joint ready for shipment

The Application

The unit was designed to handle dry sulfur gas (SO₂/SO₃) — one of the most aggressively corrosive media encountered in industrial processing. The Pressure balanced expansion joint is placed between the converter and the boiler. Operating within a uranium conversion facility, the expansion joint serves to absorb thermal growth in the piping system while maintaining zero net pressure thrust loads on the connected converter — a critical equipment in the plant where chemical reaction of the contact process takes place.

The Design

Rated for 1,196°F at +/-14.5 PSIG (Full Vacuum) and 2.75” axial movement, the 36” unit features a pressure balanced configuration: three bellows of different diameters — two line and one balancing — working in tandem to cancel out pressure-induced forces so that no axial load is transmitted to the connected nozzles. The entire assembly, including bellows, liner, and structural hardware, was fabricated from 304H stainless steel, the high-carbon austenitic grade selected for its superior creep resistance at extreme temperatures. A full-bore internal liner protects the bellows from direct gas impingement and flow-induced vibration.

The expansion joint long seams of both the pipes, as well as the bellows were all 100% Radiography examined. Other pressure retaining areas were dye-penetrant examined. The complete expansion joint examined was leak-tested after completion.

Rapid Response, No Compromises

What makes this project stand out is the timeline. The request came in as an Emergency on Sunday, US Bellows responded within minutes of the request. From receipt of order to ship-ready unit, US Bellows compressed what is typically a multi-week fabrication cycle into an emergency turnaround completing fabrication on Thursday, only 4 days from the receipt of call on Sunday— mobilizing engineering, materials, and shop resources in parallel. For a mining and milling operation, every day of downtime carries significant operational impact. Our ability to execute under that kind of pressure, while meeting all design and quality requirements, reflects the depth of experience and flexibility that sets US Bellows apart.

US Bellows Capabilities

This project highlights several core strengths that we bring to every job:

  • Emergency & rush fabrication — rapid response without sacrificing engineering and Quality
  • Pressure balanced expansion joint design — eliminating thrust loads on sensitive equipment
  • Corrosion-resistant materials expertise — selection and fabrication in stainless and high-alloy grades
  • High-temperature applications — engineered for extreme thermal and process conditions
  • Custom engineering — every unit designed to the specific demands of the application

US Bellows specializes in the design and manufacture of metal expansion joints for the most demanding industrial applications. Contact us to discuss your project.

Read More

4″ Dia. Single Expansion Joint Designed for a Chemical Facility

July 20, 2026

4" Dia. Single Expansion Joint Designed for a Chemical Facility

Type:  Single Expansion Joint with Control rods
Size:  4″ pipe
Material:  304 Stainless Steel | Carbon Steel
Design  150 PSIG at 300°F spring rate of 425 lb./in
Testing:  100% Dye-penetrant | Hydro-tested

U.S. Bellows Designed and fabricated single expansion joints for a chemical processing facility in Canada. Designed for 4-inch piping, each expansion joint accommodates 1 inch of axial movement with a spring rate of 425 lb./in. The units come with covers to protect the bellows during installation and operation. The units also have control rods to prevent any excess movement from the expansion joint and are designed to contain the pressure thrust in case of an anchor failure. The expansion joints are rated for a design pressure of 150 PSIG at 300°F, ensuring reliable performance under demanding operating conditions.

To verify quality and performance, each expansion joint underwent 100% dye penetrant examination and a hydrostatic pressure test prior to shipment, ensuring compliance with the project’s stringent quality requirements and providing the customer with a dependable, high-quality solution.

Read More

Oversized vs Same-Size Clamshell: Choosing the Right Repair for Your Piping System

July 9, 2026

clamshell

When a metallic bellows fails, the priority is restoring system integrity with minimal disruption to operations. In many facilities, the standard approach of removing and replacing the existing expansion joint is not always practical. Surrounding piping, structural steel, refractory systems, or insulation can make removal time-consuming, costly, and in some cases, simply not feasible within the available outage window.

A clamshell bellows addresses this directly. US Bellows fabricates two distinct configurations: oversized and the same size clamshells. Selecting the right one depends on the specific conditions of the repair.

This article explains how each type works, when to use one over the other, and what to consider before contacting an engineer.

What Is a Clamshell Bellows?

A clamshell bellows is a split metallic bellows assembly manufactured in two longitudinal halves. The halves are assembled around the damaged or leaking bellows and welded together,  either in the field or in the shop,  without requiring the full removal of adjacent piping, structural components, or surrounding equipment.

Clamshell bellows are fabricated in single-ply metallic bellows only. They are not suitable for fabric or rubber expansion joints, in these cases, contact us to discuss repair options. There are no inherent pressure or temperature class restrictions; each assembly is custom-designed to the material, geometry, and service conditions of the existing joint.

Note – Clamshell bellows are a temporary repair solution. They restore system containment and allow continued operation while a permanent replacement is planned.

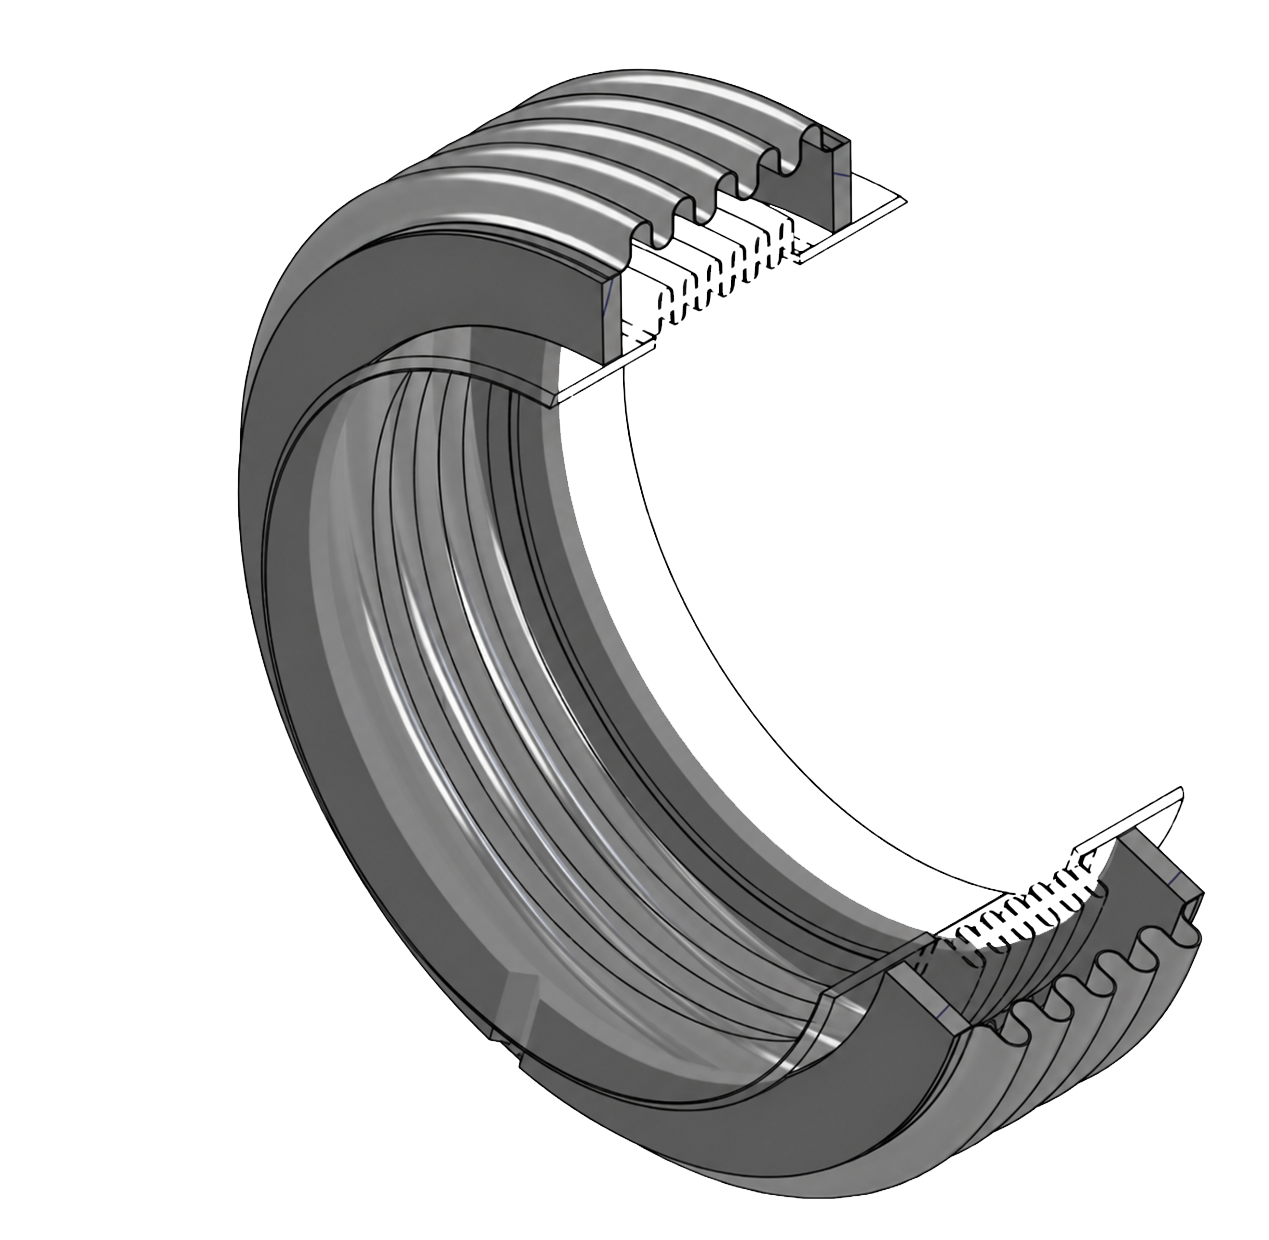
Oversized Clamshell Model
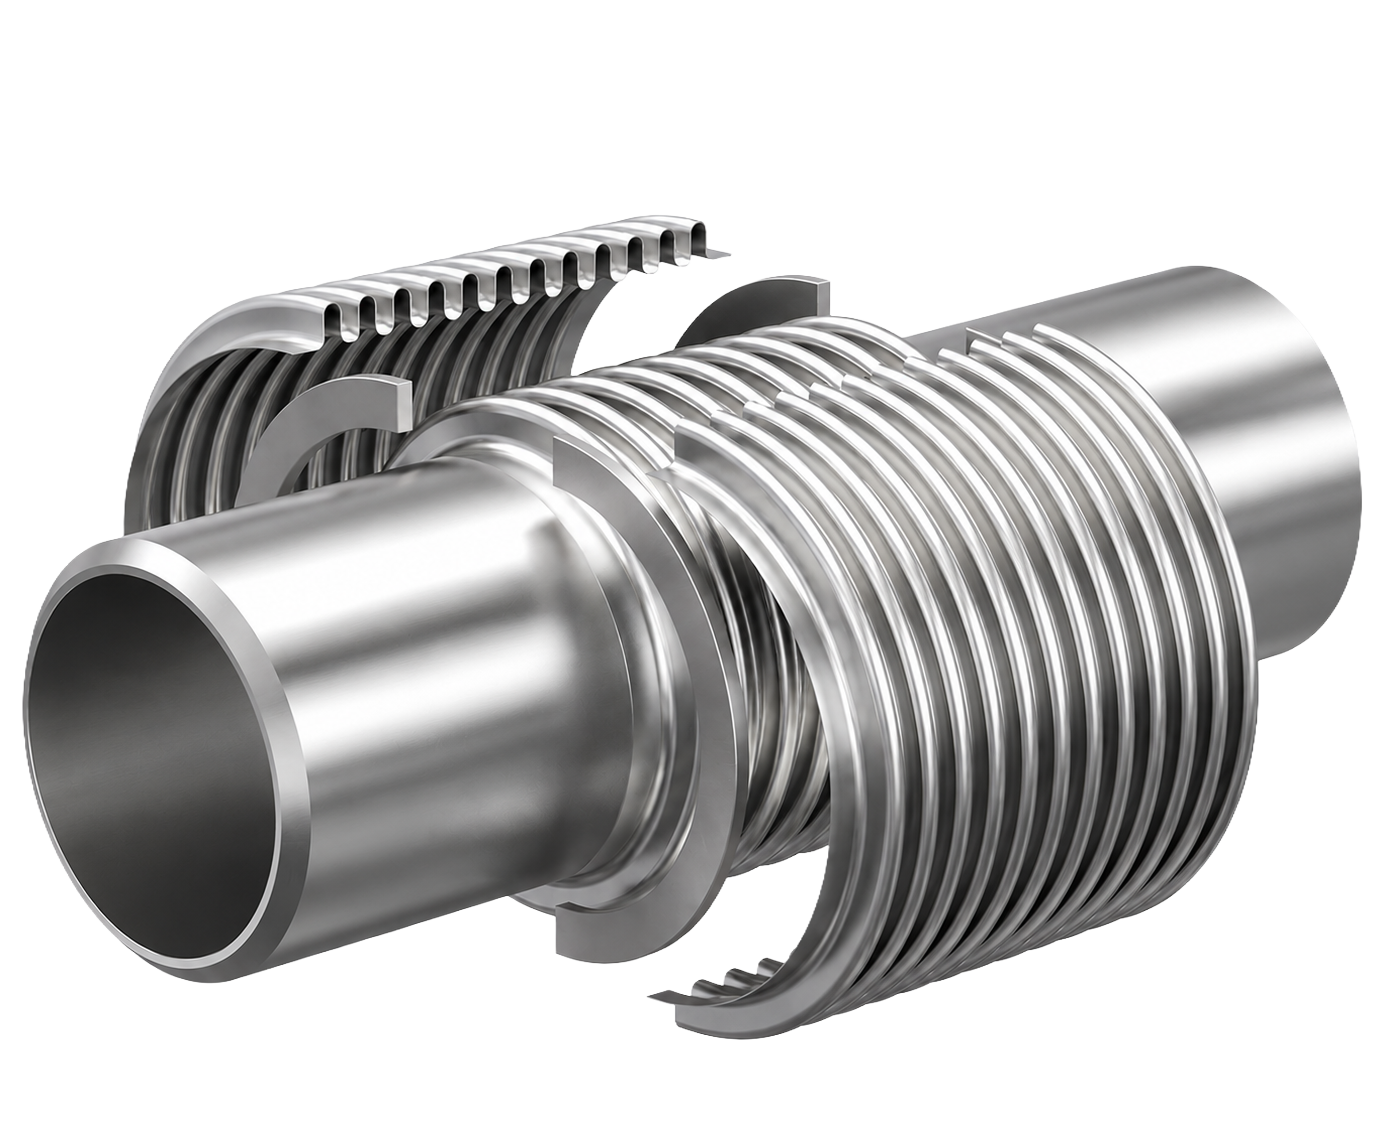
Same-Size Clamshell
Same-Size Clamshell

The Two Configurations

Oversized Clamshell

An oversized clamshell uses rings to increase the enclosure diameter beyond that of the existing bellows. The assembly is built to enclose the failed joint from the outside, without making contact with it, cutting it, or removing it. The repair is performed entirely in the field.

This configuration is used when removing the existing bellows is not practical. Large-diameter joints surrounded by permanent piping, structural steel, refractory, or insulation are typical candidates. In these situations, the cost and time required to dismantle the surrounding system can far exceed the cost of the clamshell itself. The oversized design eliminates that work entirely.

Field installation requires slow, precise welding along the longitudinal seams. Access constraints, working at elevation, and tight clearances all add to the complexity of the weld. This is the primary tradeoff of the oversized configuration: it avoids disassembly, but the field weld must be executed carefully under site conditions.

Same-Size Clamshell

A same-size clamshell is manufactured to match the dimensions of the existing bellows. It is designed for situations where the existing joint, or the equipment it is part of, can be removed and either sent to the US Bellows facility for a shop repair or replaced in the field after the original bellows has been taken out.

This configuration is better suited for turnaround scenarios. When a failed bellows is discovered during a planned or unplanned outage, and there is sufficient time to remove the joint, a same-size clamshell can be fabricated and installed with tighter quality control, full weld access, and US Bellows can provide complete ASME documentation when required.

Comparison at a Glance

Oversized Clamshell Same-Size Clamshell
How it works Rings increase the enclosure diameter to fit over the existing bellows Manufactured to match the dimensions of the existing bellows
Best suited for Large-diameter field repairs, emergencies where removing the existing joint is impractical Turnarounds where the equipment can be sent to the shop or the EJ can be removed in the field
Installation Field-welded in place around the existing failed joint Shop repair at the US Bellows facility, or field installation after joint removal
Key advantage No need to cut, remove, or disturb the existing bellows or surrounding components Tighter quality control, full weld access, and ASME documentation are more straightforward
Primary tradeoff Higher fabrication cost; field welding required under site conditions Removal of the existing joint or equipment adds time and labor
Typical application Large-diameter lines with surrounding refractory, structural steel, or insulation Heat exchangers, turnaround repairs with a sufficient outage window

How to Determine Which Configuration Fits Your Situation

The decision comes down to two questions:

1. Can the existing bellows or equipment be removed?

If yes,  and there is time in the outage window to do it, the preferred option is for a new bellows replacement to be provided. However, in cases such as heat exchangers, where disassembly would be time-consuming, a same-size clamshell is generally the more controlled repair. It allows for shop fabrication, easier welding, and straightforward ASME documentation.

If removal would require cutting permanent piping, dismantling structural supports, removing refractory or insulation, or using crane support for a large-diameter joint, an oversized clamshell avoids that work entirely.

2. What are the access conditions at the joint location?

Oversized clamshells are designed specifically for constrained conditions. If the joint is surrounded by equipment, located at elevation, or embedded in a system where adjacent components cannot easily be disturbed, field installation of an oversized clamshell is the practical path.

What US Bellows Needs to Design A Clamshell

Regardless of which configuration applies, the following information is required to start the engineering review:

  • Nominal pipe size and bellows outside diameter
  • Material and ply count of the existing bellows
  • Design pressure and temperature
  • Type of movement accommodated (axial, lateral, angular)
  • Accessibility constraints and site conditions
  • Drawings or dimensional sketches of the existing assembly, when available

For urgent repairs, US Bellows’ engineering team is available around the clock. Both configurations can be designed and fabricated on emergency turnaround schedules when the situation requires it.

Have a bellows failure or an upcoming turnaround? Contact US Bellows or schedule a meeting with an engineer to discuss which clamshell configuration fits your situation.


Read More

Elbow Pressure Balanced Expansion Joint Designed for a Chemical Processing Plant

July 7, 2026

Elbow Pressure Balanced Expansion Joint Designed for a Chemical Processing Plant

US Bellows custom-designed and manufactured an 18-inch diameter elbow pressure balanced expansion joint for a chemical processing plant used in the production of compound fertilizers. The expansion joint was engineered to accommodate thermal movement while minimizing pressure thrust loads in the piping system, making it well suited for the plant’s nitrogen oxide process.

The assembly measured 83-3/8 inches from the weld end to the centerline of the elbow. The body, pipe, covers, and tie rods were fabricated from 304L stainless steel, while the bellows and internal liners were manufactured from 321 stainless steel for enhanced high-temperature performance. The unit was designed to accommodate 1/2 inch of axial compression and 4-1/8 inches of lateral movement while operating at 600°F and 125 psig.

As part of PT&P’s quality assurance program, the completed assembly underwent 100% dye-penetrant examination and a hydrostatic pressure test at 190 psig prior to shipment to verify structural integrity and compliance with project specifications

Read More

Fabric Expansion Joint Custom Designed for an Exhaust Application in a Gas Turbine Facility

June 24, 2026

128016a1
US Bellows custom-designed and manufactured this 153″ x 55″ x 21″ fabric expansion joint for an exhaust application at a gas turbine facility overseas. The expansion joint features a carbon steel frame and liner with a protective painted finish. The flexible element consists of a reinforced neoprene fabric belt designed to accommodate system movement while maintaining reliable performance under demanding operating conditions.

The assembly was engineered for a pressure rating of ±100″ water column and operating temperatures ranging from -20°F to 600°F. Prior to shipment, the expansion joint underwent a 100% dye-penetrant examination and paint thickness inspection to verify compliance with project quality requirements.

US Bellows specializes in the design and manufacture of custom fabric expansion joints for gas turbine exhaust systems, power generation facilities, industrial ducting, and other applications requiring flexibility, vibration isolation, and thermal expansion compensation.

Read More
1 2 3 19